
Choosing Your Microstop Countersink Cage
By the Wescon Engineering Team · Last updated September 12, 2026To choose a microstop countersink cage, work through four choices in order: the cutter, the series, the shank and the footpiece. This guide covers each one, with the Wescon series that fit common aircraft jobs.
Countersinking is the process of preparing a hole so a fastener sits flush with the surface. A microstop countersink cage, also written micro stop, controls how deep the cutter goes. Depth control keeps fastener rows flush on the metal and composite panels of aircraft wings and fuselages, so the surface stays aerodynamic.
A countersink that is too deep or too shallow keeps the fastener from seating correctly. Over time, this weakens the joint and can cause panels to separate.
A microstop, also called a countersink cage, attaches to a handheld drill motor, holds the countersink cutter at a fixed setting, and helps control the travel depth of the cutter to a set length. Once set, it holds that depth across hundreds or thousands of holes without drifting. This consistency is why microstops are the standard tool aerostructure engineers use for countersinking work.
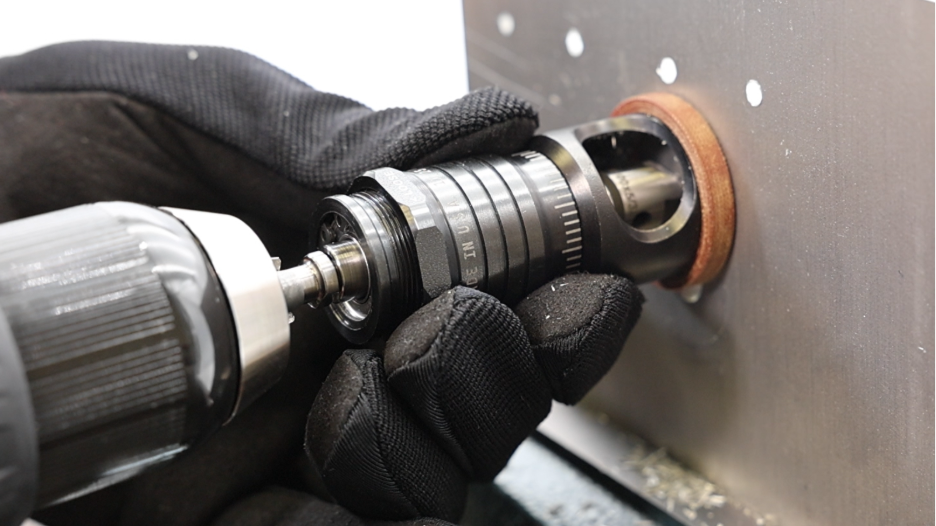 Photo: Wescon Industries Inc., CC BY 4.0
Choosing the right microstop depends on a few parameters your job demands.
How to Choose Your Microstop
Step 1. Determine the Correct Cutter
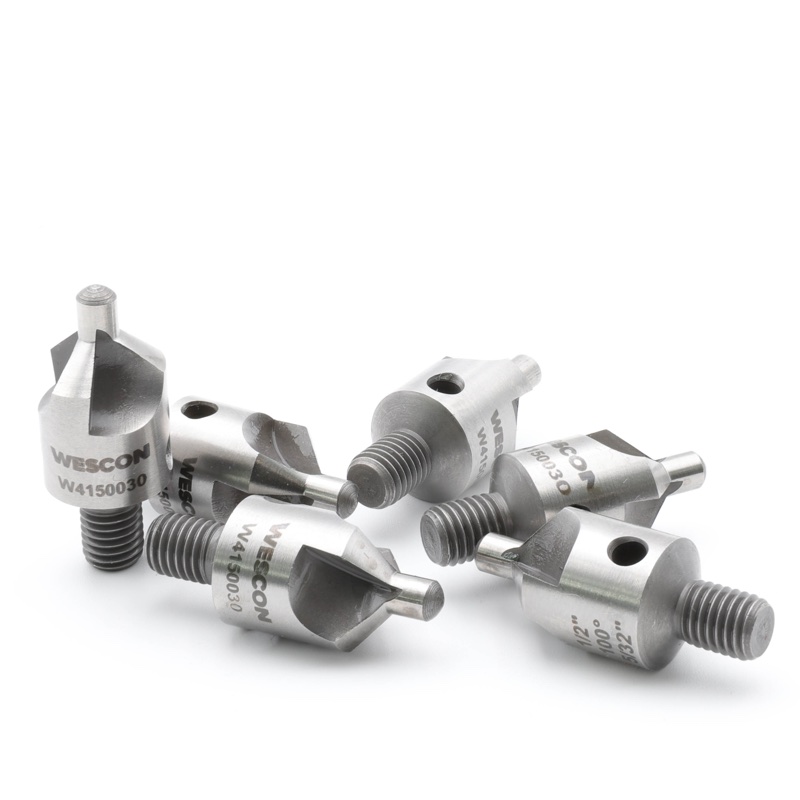 Photo: Wescon Industries Inc., CC BY 4.0
The main purpose of the microstop is to hold a cutter meant for countersinking; the cutter that’s in use is one of the main factors that will help you identify which microstop can hold it. For that reason, you need to choose the right cutter. What you need to know are:
- The dimensions of the fastener or countersink rivet, since they determine the cutter needed to create a countersunk hole where the fastener sits flush with the surface.
- The material of the work surface or aerostructure panel, since it determines the material of the cutter required
- The installation standards or specifications for the job
Our microstops can hold:
- Imperial threaded cutters with 10-32, 1/4"-28, 3/8”-24 or 7/16”-20 threads
- Metric threaded cutters with M6x1, M8x1 or M10x1 threads
Step 2. Determine the Correct Series
Fasteners sit in different places. Some are easy to reach; others might be in tight or obscure areas. Because of this, no single microstop configuration works for every job. The right series depends on your access to the jobsite.
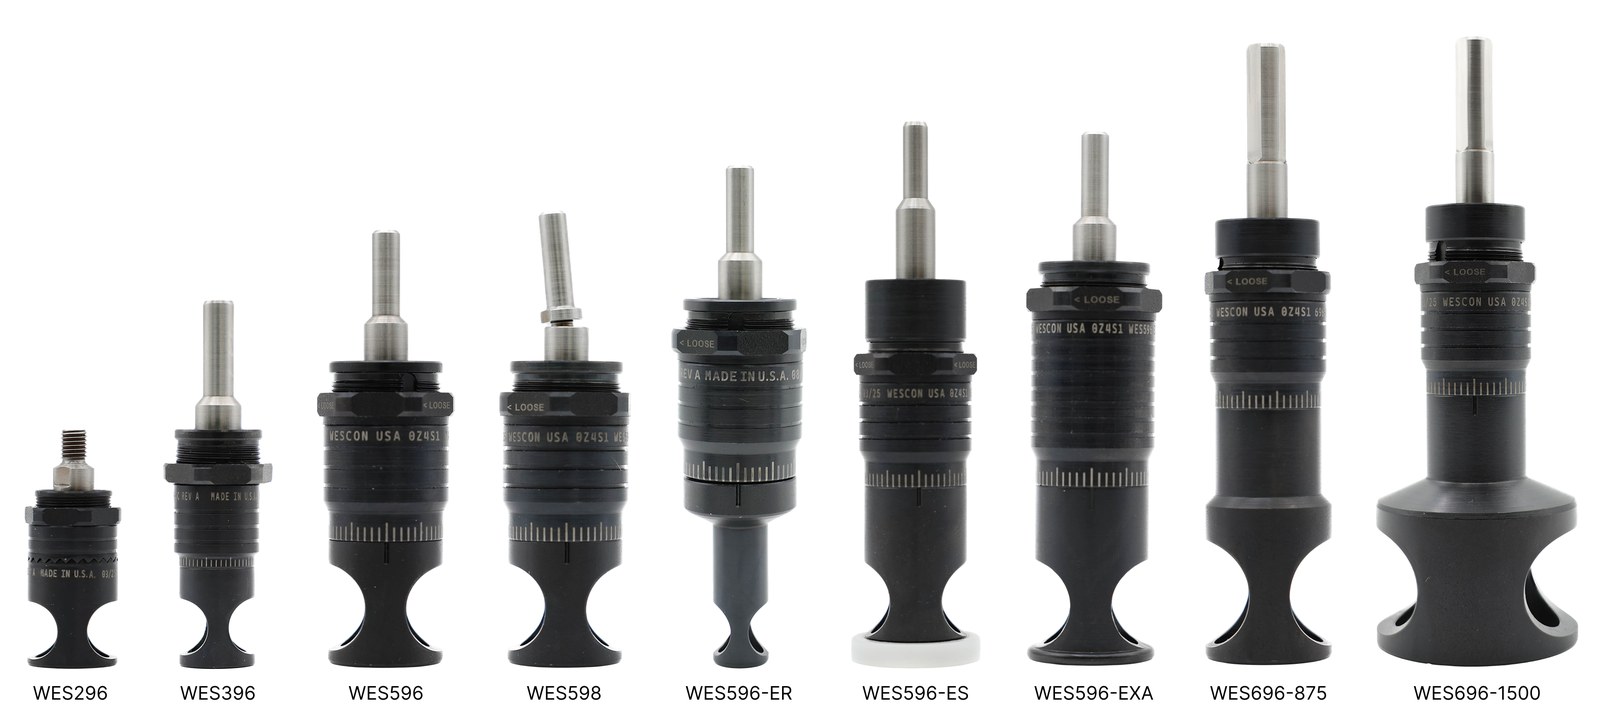 Photo: Wescon Industries Inc., CC BY 4.0
| Series | Description |
|---|---|
| WES296 | Fits right-angle drill motors, for areas you cannot reach in a straight-in position. |
| WES396 | Built for tight spaces, with smaller cutters and a smaller footprint. |
| WES596 | The industry standard. Best for most work surfaces with easy access. |
| WES598 | Has a 10-degree pivoting shaft that angles into hard-to-reach holes a straight shaft cannot reach. |
| WES596-ER | Built to reach deeper into tight areas and hard-to-reach sections of an airframe. |
| WES596-ES | A longer-stroke unit built for special, customer-specific operations that need a longer cutter. |
| WES596-EXA | Built for jobs with many different cutter lengths, with extended adjustment to handle multiple tasks in one unit. |
| WES696 | Built for larger diameter cutters. |
| TL | Built to house Taper-Lok cutters, for drilling holes that fit Taper-Lok fasteners used in high-strength attachment points. |
Once you know your cutter and the microstop use case, you can choose the right skirt option. Some skirts have a limit on the cutter size they can hold.
Our standard skirt options cover most cutter capacity needs. If your job needs something outside that range, contact us and we will help you find the right skirt or build a custom option.
Step 3. Match Your Shank to Your Drill Motor
Not every drill motor used for countersinking is the same. That is why microstops come with different shank options. Based on your drill's chuck type, you can choose between:
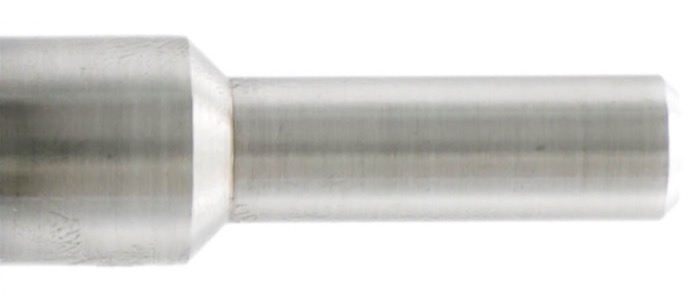 Photo: Wescon Industries Inc., CC BY 4.0
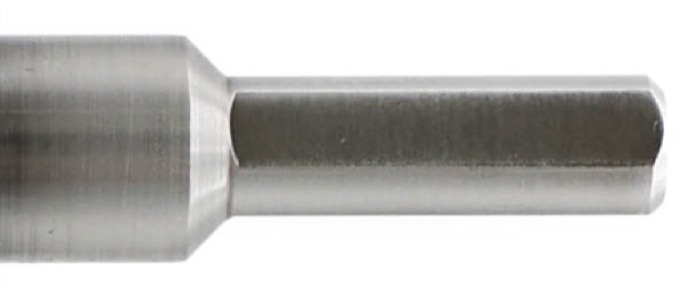 Photo: Wescon Industries Inc., CC BY 4.0
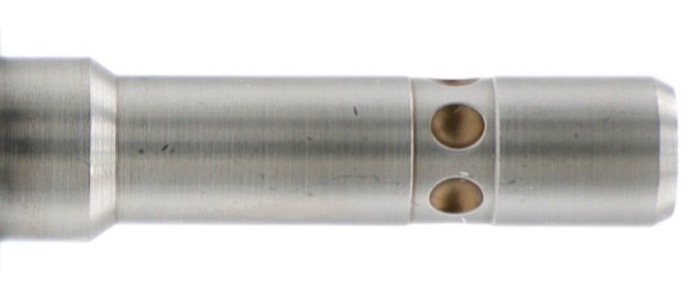 Photo: Wescon Industries Inc., CC BY 4.0
- Round (Blank): A standard shaft that fits a standard 3-jaw chuck.
- Tri-Flat (TF): Also fits a 3-jaw chuck, built for heavy countersinking on steel and larger cutters, where applications require better grip; preferred in situations where a round shank might slip in the chuck.
A Quick-Change (QC) configuration is also available. It needs a QC chuck adapter, such as our WES1750 Series, mounted on a threaded drill motor. This system mostly applies if you work at a Boeing facility or as a Boeing subcontractor, where it is the standard.
Long threaded shank (TSL) options are also available. However, these are custom-built for threaded motors or chucks upon request.
Step 4. Protect the Work Surface with the Right Footpiece
The footpiece is what makes contact with your work surface. Some jobs need no footpiece. On a finished surface, a nylon foot gives the most protection.
For a full breakdown of footpiece materials and how to pick the right one, read our guide: How to Prevent Surface Marring During Precision Countersinking.
Need to pull chips and carbon fiber dust away while you countersink? See Microstop Vacuum Skirts: FOD Extraction When Countersinking.
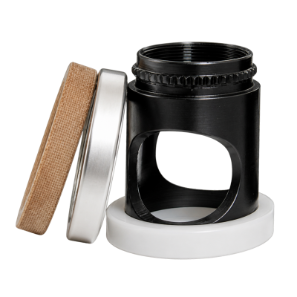 Photo: Wescon Industries Inc., CC BY 4.0
Every Wescon series, with its cutter thread and shank options, is in the microstop countersink cage catalog.